Connected devices, intelligent software, and constant data gathering are revolutionizing how industrial facilities operate through the implementation of smart factories. Among the most important tools used for smart factory evolution is remote monitoring, which enables tracking of machines and production status without exclusively depending on manual checks. Offering timely information and fast decision-making opportunities, this technology plays a big role in making factories more productive and resilient. Here are five major benefits of remote monitoring.
Enables Real-Time Equipment Visibility
Normal inspections typically only give periodic views of the condition of machines. Monitoring remotely allows for the constant flow of data from a machine’s operation, providing greater insight into what is going on at the factory. Machines’ operation can be monitored by using various sensors that measure different variables such as vibrations, temperature, pressure, speed, and energy consumption. Remote monitoring platforms collect data from sensors, making analysis easier. Abnormal data will be easily found without having to wait for the next planned inspection. The system makes it possible to control the equipment spread all over the facility and even several facilities.
Improves Equipment Life and Reliability
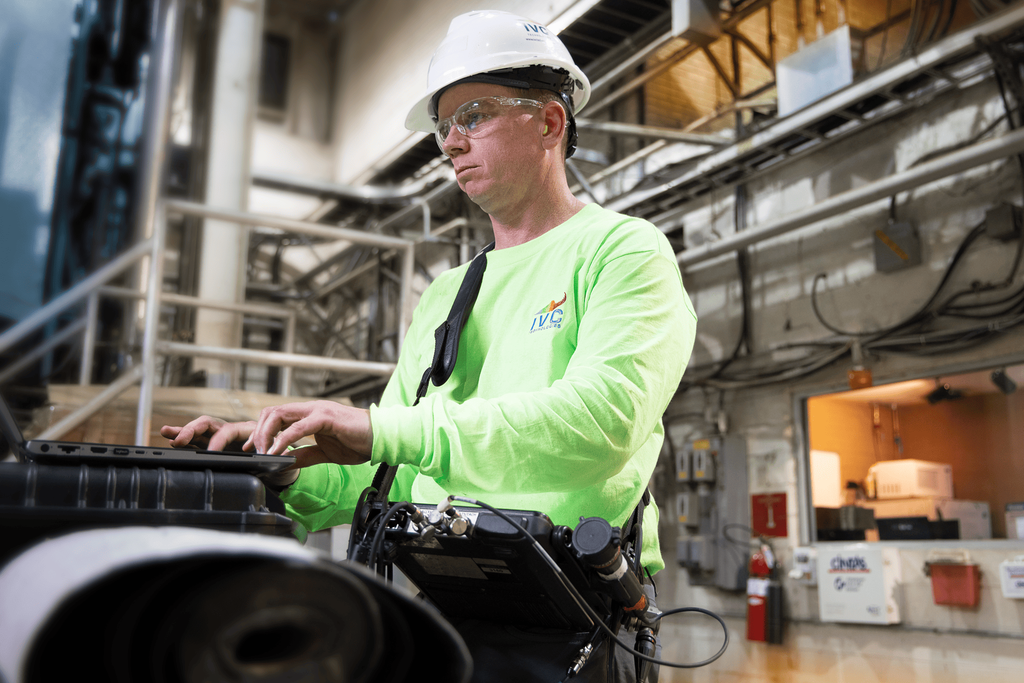
Any kind of equipment breakdown could disrupt manufacturing operations, result in repair costs, and further add to the burden of maintenance staff. Remote monitoring allows predictive maintenance through detecting any variations that could be indicative of potential mechanical faults. An increase in the amount of vibrations could suggest mechanical problems such as bearing failure, unbalance, misalignment, and others. Maintenance personnel can investigate these warning signs and address developing faults before severe damage occurs. Manufacturers seeking to strengthen this approach can choose excellent remote vibration monitoring services that provide specialized analysis and useful condition data. Early intervention reduces unnecessary wear, supports more informed maintenance schedules, and can extend the useful operating life of critical machinery.
Reduces Unplanned Downtime
Production stoppage may be very costly, especially if there is a shutdown of a crucial piece of equipment. By utilizing remote monitoring, there is a possibility of decreasing such risks by providing early signs of any deviations from normal operation. Rather than realizing the fact of a problem when there is already a malfunction, personnel will receive notifications whenever the measurements show something that is not in accordance with the set boundaries. There is an option to plan an inspection, repair, or replacement of components at a convenient moment for the facility’s work schedule. Production planners can also coordinate service activities around operational demands, reducing disruption to manufacturing schedules.
Strengthens Data-Driven Decision-Making
Smart factories need correct information to make proper decisions about their operation. Remote monitoring helps to gather the work of the machinery in a form that can be analyzed together with the maintenance data, production data, and past performance of the factory. Trends over time might help discover recurring malfunctions, inefficiencies in the work of the machines, and components that frequently cause problems. Managers can take all this into consideration when they make decisions about their maintenance priorities and other issues. The data may also be helpful for comparing production lines within an organization and finding what requires additional research.
Supports Safer and More Efficient Operations
The remote monitoring of equipment may also ensure greater safety among workers, as it can help eliminate the need for workers to visit dangerous places frequently. Sensors attached remotely can gather data about how machines work in high-temperature, high-pressure, and high-speed situations. It will be possible for teams to assess if there is a need for an actual physical inspection based on that data. Remote monitoring can also assist in identifying inefficient working patterns of the equipment, like unnecessary power consumption or abnormal machine performance. Such issues can be sorted out, leading to efficient usage of resources along with providing a safe working environment.
The idea of remote monitoring has become an essential part of the modern smart factory. The ability to see all processes continuously, increase reliability, decrease downtime, improve data analysis, and ensure safety shows how remote monitoring can change industrial maintenance and manufacturing. With the further development of sensors, analytics, and industrial connectivity, companies will be able to utilize remote monitoring to create more resilient factories. The most important thing about remote monitoring is not only collecting data but acting on it.
